

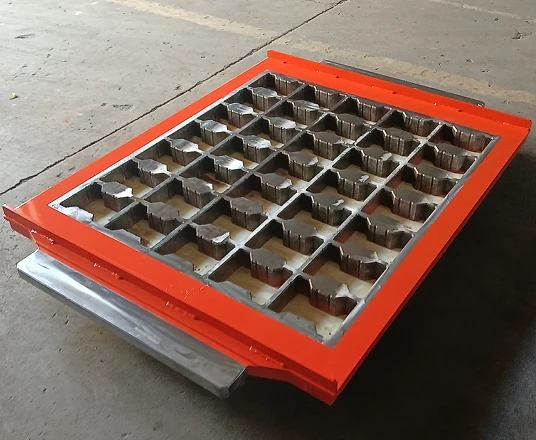

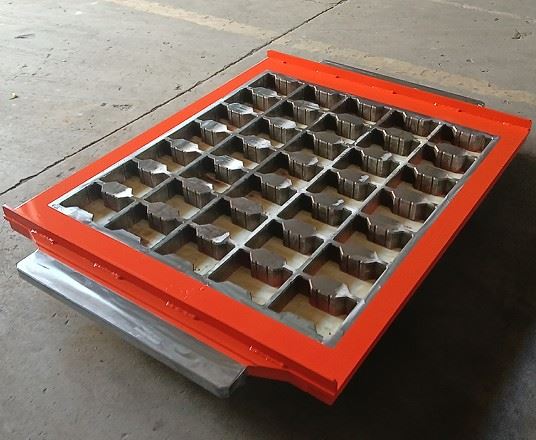
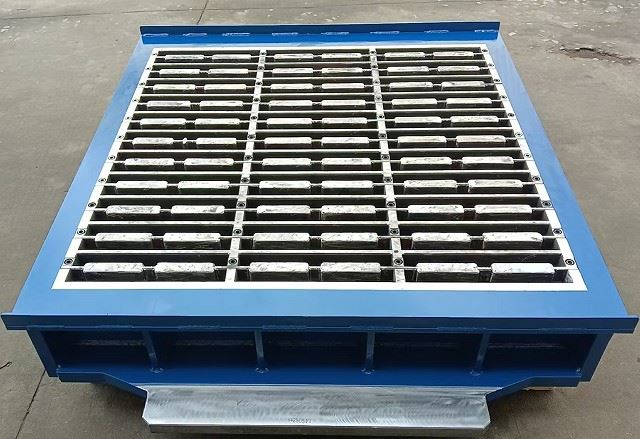
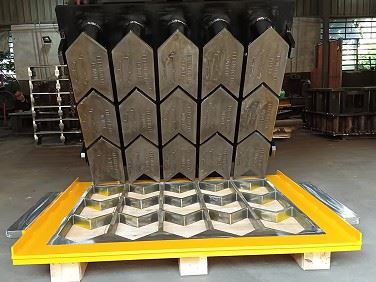
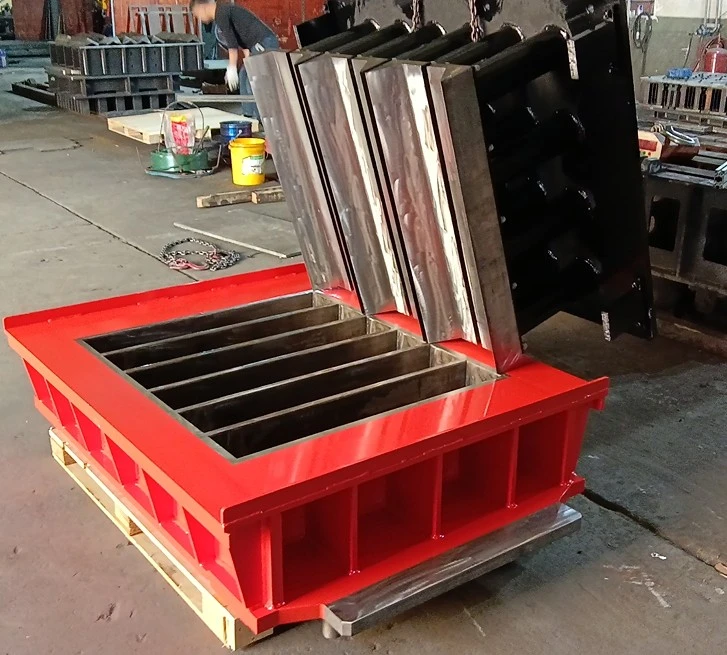
Interlocking Paver Block Mould Design
2.Hardness for shoes:HRC59-62
3.Carburized layer thickness:1.3-1.5mm
4.Unilateral clearance between presser foot and mold cavity: 0.2 mm ≤ Unilateral clearance ≤ 0.4mm
5.Flatness of the whole board: ≤ 0.5mm
6.Deviation in length and width dimensions of a single cavity model: -0.3 to+0.3mm
7.The dimensional deviation of the height (filling depth) of the lower model cavity is ± 0.5mm
Send Inquiry
Product Details ofInterlocking Paver Block Mould Design
interlocking paver block mould design
Precision Engineering for Durable, High-Performance Pavements
At Fujian Unik Mould Technology Co., Ltd., we approach interlocking paver block mould design as a sophisticated engineering discipline that merges material science, precision manufacturing, and field-proven principles. Since our founding in 2010 in Quanzhou, Fujian-a region renowned for its manufacturing excellence and strategic position on the Maritime Silk Road-we have dedicated ourselves to advancing the technology that shapes modern hardscape surfaces . Our interlocking paver block moulds are engineered to produce concrete units that mechanically engage with adjacent pavers, distributing loads across entire pavement surfaces while accommodating thermal expansion, drainage requirements, and aesthetic demands.

Fundamental Design Objectives
Every interlocking paver block mould must satisfy multiple performance criteria simultaneously. The interlock geometry-whether dog-bone, S-curve, X-shape, herringbone, or custom profile-must provide sufficient mechanical engagement to prevent vertical displacement under traffic loading while allowing adequate horizontal flexibility for thermal movement . The mould cavity must produce faces sufficiently smooth for comfortable pedestrian traffic, yet textured enough for slip resistance in wet conditions.
Our interlocking paver block mould design process begins with comprehensive CAD/CAE integration. Finite element analysis allows our engineers to simulate stress distributions under actual wheel loads, evaluating contact pressures at interlock interfaces and identifying potential stress concentration points that could lead to corner cracking or edge spalling . This computational approach enables optimization of interlock depth, flank angle, and transition radii before any steel is cut, ensuring that the final mould geometry delivers superior performance across its entire service life.
Material Selection and Metallurgical Excellence
The foundation of durable interlocking paver block mould performance lies in material quality. We specify vacuum-degassed alloy tool steels such as Cr12MoV, 9CrSi, and 42CrMo, materials offering optimal combinations of hardness potential, wear resistance, and toughness . These steels undergo multi-directional forging that refines cast grain structures into uniform, fine patterns essential for withstanding the abrasive action of quartz-rich concrete mixes.
Our heat treatment processes are equally critical to mould performance. Preliminary heat treatment includes spheroidizing annealing, creating uniformly distributed carbide networks that respond predictably to subsequent hardening processes . Through vacuum quenching at 980 °C followed by tempering at 580 °C, and carburizing that hardens the surface layer to HRC 58-62 while maintaining a tough core at HRC 35-40, every interlocking paver block mould achieves consistent metallurgical performance with minimal dimensional distortion . This dual-phase hardness prevents cracking from vibration impact while resisting abrasion from concrete aggregates, delivering an expected operational lifespan of 80,000 to 120,000 cycles under normal production conditions .


Precision Manufacturing for Exact Geometry
Interlocking pavers require exacting dimensional accuracy. Imperfections in the mould result in uneven gaps, poor locking, increased waste, and premature pavement failure. UNIK's interlocking concrete paver moulds are produced through several controlled processes that ensure every cavity produces pavers with identical profiles, smooth release, and low surface defects .
Our CNC machining technology guarantees exact cavity dimensions with tight tolerances of ±0.1mm and a surface finish of Ra 1.6 or better . Critical design details include a 1.5° draft angle per side for smooth hydraulic ejection and prevention of under-cut stress, 3-5mm radius on all internal corners to eliminate stress concentration points that could lead to fatigue cracks, and 0.3mm pre-compaction allowance to accommodate steel rebound during pressing .
Large-scale Coordinate Measuring Machine (CMM) capability-rare among domestic mould manufacturers-enables full three-dimensional verification of cavity geometries . This ensures that critical dimensions such as unilateral clearance between presser foot and mould cavity (0.2-0.4mm), flatness of the whole board (≤0.5mm), and dimensional deviation of each cavity (-0.3 to +0.3mm) consistently meet design specifications .
Commitment to Customer Success
Choosing UNIK means choosing a partner dedicated to your operational efficiency. We do not offer generic, off-the-shelf moulds. Every order begins with your specific paver design and machine specifications. We provide comprehensive support including maintenance guidance, spare parts availability, and technical assistance to ensure optimal performance and longevity of your moulds .
For paving block moulds that combine manufacturing precision, innovative engineering, and responsive service, Fujian Unik Mould Technology Co., Ltd. stands ready to elevate your concrete products to new levels of quality and market distinction. Contact us today to discuss your interlocking paver block mould requirements. From initial concept through field-proven performance, our design process ensures that every mould delivers value across its entire service life
Hot Tags: interlocking paver block mould design, China interlocking paver block mould design manufacturers, suppliers, factory, Brick Paver Mould, Cement Paver Mould, Grass Paver Mould, Interlocking Paver Mould, Mould for Paver Block, Paver Block Mould
Previous
No InformationSend Inquiry
